That sick feeling hits the moment you spot it — a crack splintering across your carbon fiber frame, a soft spot where solid structure used to be, or a chunk missing from a part you paid serious money for.
Don’t write off your wallet just yet. Most people don’t know this: carbon fiber repair is something you can learn. With the right epoxy resin and a solid carbon fiber repair process, a clean fix can bring structural integrity back close to factory spec.
This guide covers every stage. You’ll go from diagnosing the damage type to laying patches, curing the repair, and finishing clean. By the end, you’ll have a repaired part — not just a rough idea of how it works.
What Type of Carbon Fiber Damage Do You Have? (Damage Assessment Guide)

Misreading the damage is how repairs fail. You sand down what looks like a surface scratch, apply a patch, and three months later the same spot delaminates. The real problem was underneath the whole time.
Carbon fiber fails in six distinct ways. Each one needs a different fix.
Surface scratches — the clear coat is scuffed, but the fiber weave underneath is untouched. Cosmetic only. No structural concern.
Surface cracks — hairline fractures running through the matrix resin. Stress or impact pushed the top layers past their limit.
Delamination — the plies have separated from each other. You’ll see it as a raised area, a dull patch, or a faint bubble under the surface. A 2023 CompositesWorld report found this is the most common structural failure in CFRP components.
Through-cracks and fractures — damage that has gone through multiple layers. Time, stress, and repeated loading are the main causes.
Holes and punctures — full penetration. Impact damage. The composite is compromised all the way through.
Broken fibers — individual filaments snapped from abrasion or impact. The weave loses its tensile strength. Load transfer becomes uneven across the part.
How to Identify Which One You Have
Start with a slow visual pass in good lighting.
-
Fine lines on the surface → matrix crack
-
Dull or raised patches → delamination
-
Visible holes or pitting → puncture or void
-
Superficial scuffs → clear coat only
Then tap it. Run a coin across the suspicious area and listen. A solid tick means healthy laminate. A hollow thud means the layers have separated — classic delamination.
Load-bearing parts need a closer look. Ultrasound and thermography pick up internal flaws that visual inspection misses. Acoustic Emission testing can spot active fiber breakage as it happens.
Repair or Replace?
|
Repair It |
Replace It |
|---|---|
|
Small cracks in non-load-bearing areas |
Damage in high-stress structural zones |
|
Superficial scratches |
Shattered or badly broken fibers |
|
Minor delamination, non-critical zones |
Deep delamination with core separation |
|
— |
Epoxy cracking throughout the part |
Damage in a primary load path — a bike frame’s chainstay, a carbon wheel’s spoke bed — is not a repair situation. Replacement is the right call. Impact damage accounts for 45% of carbon fiber wheel failures. Most of those started as damage that looked manageable from the outside.
Get the assessment right first. Everything that follows depends on it.
Tools and Materials You Need for Carbon Fiber Repair

Get this part wrong and nothing else matters. The quality of your repair lives or dies with what’s on your workbench before you start.
Here’s the full breakdown — no padding, no extras you’ll never use.
Basic Tools
-
Scissors or rotary cutter — trim carbon fiber cloth with clean, precise cuts
-
Sander with 60, 240, 320, and 400-grit discs — surface prep needs a full progression, not shortcuts
-
Sandpaper (80–400 grit) — rough out at least 2–3 inches beyond the damage edge
-
Brushes and rollers — spread resin evenly, no pooling
-
Spatula — spread the epoxy-glass bubble mix without dragging or lifting
-
Small mixing containers and sticks — blend resin and hardener at a consistent ratio. Most systems run 1:1, so measure carefully every time
Specialized Tools
-
Vacuum pump and bag — pulls air out of the layup. This improves resin distribution and removes weak spots from the finished repair
-
Masking tape — protects everything outside the repair zone
-
Plastic sheeting — covers wet epoxy and pushes out surface bubbles during cure
Core Materials
-
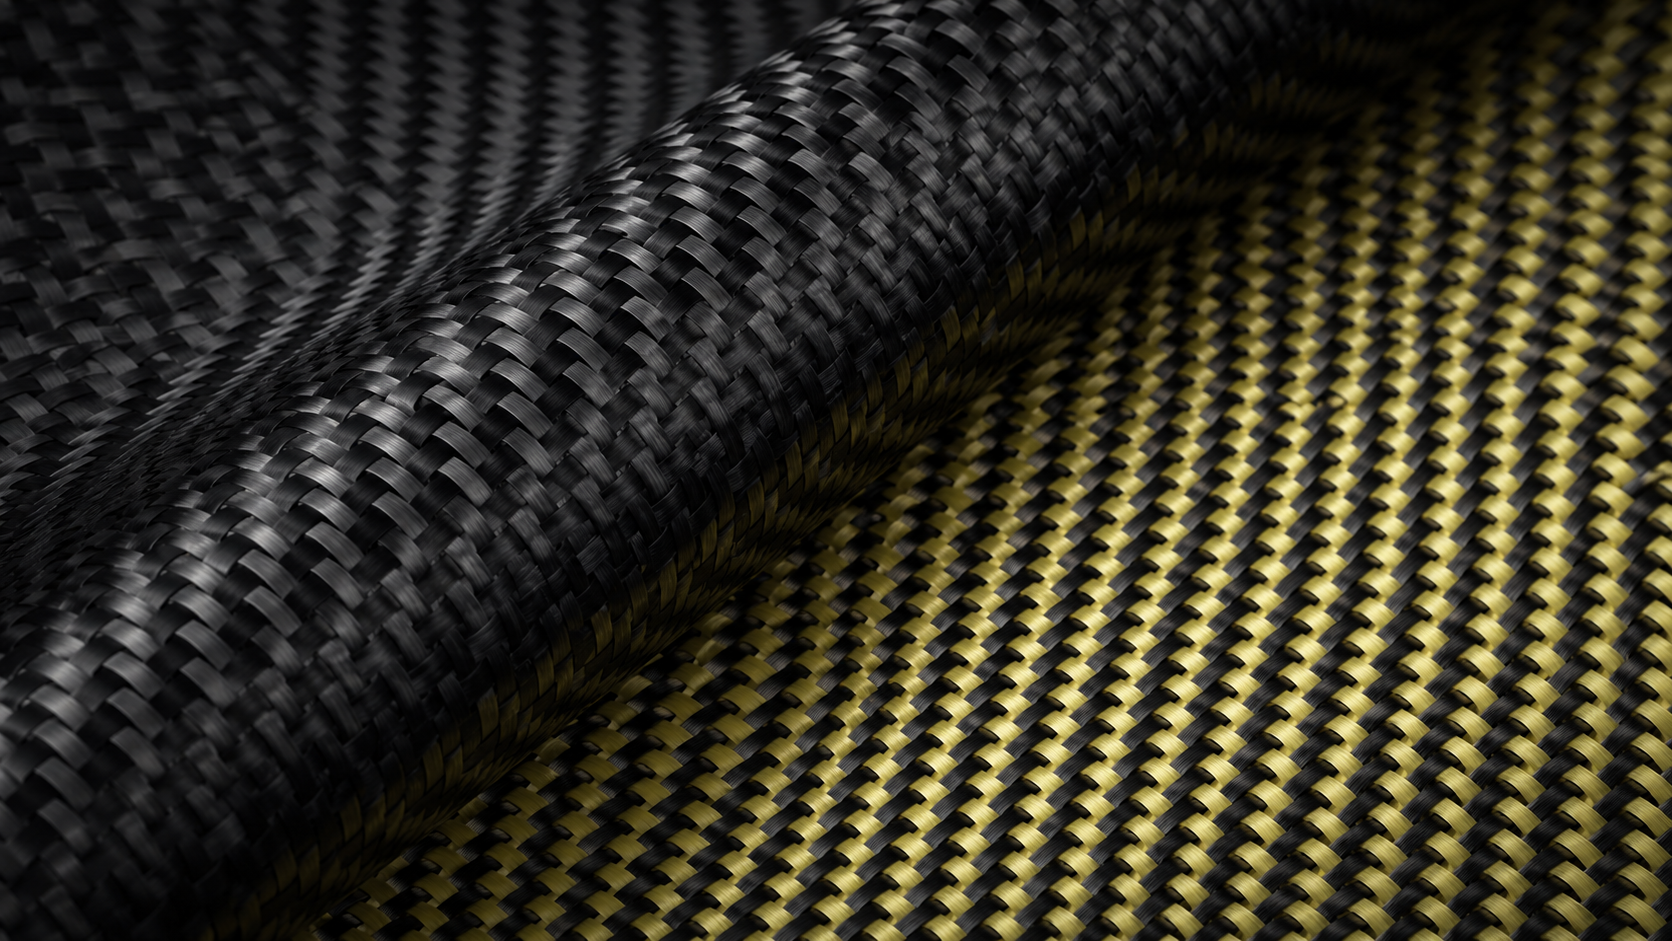
Carbon fiber fabric — woven cloth gives multi-directional strength. Unidirectional works where the load runs one way. Cut your pieces small-to-large. The smallest patch goes down first. Each layer after that overlaps wider, giving you a smooth, gradual blend
-
Epoxy resin + hardener — the structural backbone of every carbon fiber patch repair. Mix in glass bubbles for a thicker filler. It won’t sag or drip on vertical surfaces
-
Glass bubbles — mix these into epoxy to build a smooth, workable base coat. Apply this before any fiber layers go on
-
Black pigment (optional) — add this to your epoxy so it matches the color of the surrounding carbon fiber weave
-
Alcohol — wipe the surface clean before the final coat, no exceptions
-
Clear matte or gloss spray — match this to the original finish. It goes on last as your protective top layer
Cure Time Benchmarks Worth Knowing
Rushing cure time is the single most common reason DIY repairs fail.
-
Initial epoxy coat: overnight minimum
-
Each filler coat: 24 hours, then sand with 240–400 grit before the next layer
-
Final finish sanding: work up through 320 → 400 → higher for a clean result
First time sourcing materials? Pre-assembled carbon fiber repair kits bundle resin, hardener, and cloth together. They’re a solid starting point that takes the guesswork out of buying each item separately.
Step 1: Clean and Prepare the Damaged Area
Preparation isn’t the glamorous part of carbon fiber repair. It’s also the part that determines whether your patch holds for years or fails in months.
The rule is simple: epoxy won’t bond to contamination. Grease, oil, dust, wax — any of it sitting between the resin and the substrate creates a weak interface. The fiber patch goes on fine. That bond underneath? It’s already shot.
Here’s how to do it right.
Start with a degreasing wipe-down. Use isopropyl alcohol on a clean cloth. Work outward from the damage center. Don’t scrub in circles — you’ll push contamination back into the area you just cleaned. One direction, fresh cloth, repeat.
Sand the damaged zone and the surrounding area. Go 2–3 inches beyond the visible damage edge. Use 80-grit to rough up the surface and break through any clear coat or paint. You’re not trying to sand it smooth — you want mechanical bite for the resin to grip.
Remove all sanding dust before you go further. Wipe again with alcohol. Let it flash off and dry out. Applying resin to a damp surface brings back the same contamination you just spent ten minutes clearing out. Don’t undo your own work.
Check your surface one more time under direct light. Drag your fingertip across it. It should feel a little rough and dry — no slick patches, no residue.
Clean surface. Everything else builds from here.
Step 2: Cut and Fit the Carbon Fiber Repair Patches
Measure twice, cut once — that rule exists for a reason. Carbon fiber cloth does not forgive mistakes the way denim does.
Your patch must extend well beyond the damage boundary — not just cover it. The resin bond needs clean, undamaged fiber on both sides to transfer load. A patch that just clears the crack edge is already failing.
How far out do you go?
-
Minor damage (under 2 inches): overlap 1–2 inches beyond the damage edge in every direction
-
Larger defects (over 2–3 inches): extend at least 4 inches (102 mm) beyond the defect boundary
-
Not sure? Cut bigger — you can always trim back after placement
The layering logic matters here. Do not cut one big patch and call it done. Cut multiple pieces, sized small to large:
-
Innermost layer — sized to fit the repair area with a precise match
-
Each subsequent layer — overlaps the previous by 5–10 cm or 10% extra coverage
This graduated stack creates a smooth load transition instead of a hard stress edge. That edge is where single-patch repairs crack first.
Cut clean or cut nothing. Use a rotary cutter or a sharp Stanley knife on a firm surface. Sharp scissors work for smaller pieces. Keep the blade moving at a consistent pace — hesitation drags fibers out of alignment. It also leaves frayed edges that will not wet out with resin the way they should.
For the damage cutout shape: round your corners. Circular or oval outlines remove the stress concentration that square corners create. Cut your patches to match that shape, then add your overlap margin from there.
One last thing — cut all your patches before you mix any resin. Once the clock starts on epoxy pot life, fumbling with fabric and scissors eats into cure time you cannot get back.
Step 3: Mix and Apply Epoxy Resin
The ratio is everything. Get it wrong and you won’t know until the repair is soft, sticky, and cured into a useless mess.
Epoxy resin is a two-part system — resin and hardener. They don’t cure by drying. They cure by reacting with each other. That reaction depends on the correct ratio. Too much hardener and the finished repair goes malleable. Too much resin and the surface stays tacky no matter how long you wait. Off-ratio means bad crosslinking. The molecular structure never locks in. Your structural repair fails before you’ve laid a single patch.
Know your system before you mix anything.
Most carbon fiber repair epoxies run at either 2:1 (100g resin to 50g hardener) or 1:1 (equal parts by volume). Some specialty systems work differently. Entropy CLR/CLF uses a weight-based ratio of 100:47 — for every 1 oz of resin, you need 0.47 oz of hardener. The minimum batch size is 1.47 oz total. Don’t guess. Read the datasheet for your specific product.
Mixing Procedure
-
Pour resin first, then hardener into a clean, marked container — or weigh on a digital scale
-
Stir for 2–3 minutes minimum, scraping the sides, bottom, and corners as you go
-
Larger batches (over 9 oz) need more time — don’t rush the mix
-
No streaks means ready — uniform color and consistency throughout
Mix it and use it right away. Pot life starts counting down the moment both components touch.
Application
Load your brush or roller and work the epoxy into the repair zone in firm, even strokes. No pooling. No puddles. Thin, consistent coats build a stronger bond than one heavy pass.
The mixed resin goes on first as a base coat. This is where your glass bubbles come in — use them to fill a void or level an uneven surface. Saturate the base, let it tack up a bit, then lay your first patch straight into the wet resin.
Step 4: Curing — How Long and What Conditions Matter
Epoxy doesn’t care about your schedule. It cures on its own timeline. Two things control that timeline: temperature and humidity.
The sweet spot is 70–75°F (21–24°C) with humidity below 40%. Inside that range, your repair cures at a steady pace and reaches full structural strength.
Step outside it and things get complicated fast.
Temperature effects:
– Below 65°F (18°C): cure rate slows — add hours, sometimes days
– Above 80°F (27°C): cure speeds up, but pot life shrinks. You lose working time
– Every 10°C drop cuts cure rate by about half
Humidity is the one people underestimate. Push above 60% relative humidity and certain epoxy types can take ten times longer to cure — days instead of hours. Even a 0.1% rise in moisture content can stretch cure time by 30%. That’s not a minor delay. It can derail an entire repair window.
Don’t force it if conditions aren’t right. Wait it out. A cure that’s been rushed or cut short leads to a weak repair — one that may look fine on the surface but fail under load.
Step 5: Sanding, Filling, and Finishing the Repair
The repair is cured. Now the real visible work begins.
Sanding isn’t just cleanup — it decides whether the final surface holds up and looks smooth. Rush this stage and you lock every flaw in place.
Work through the grit sequence. Don’t skip steps.
-
80-grit — remove excess filler, rough-shape the repair zone, blend the patch edges down
-
180-grit — refine the shape in a 45° crisscross pattern. This catches low spots that straight-line sanding leaves behind
-
320-grit — bring the surface to primer-ready smoothness. Use a sanding block for even pressure
-
600-grit — feather the edges where the repair meets the surrounding material. This gives you clean primer adhesion
Before each new grit pass, spray on a guide coat — a thin layer of contrasting color. Sand it off. Anywhere the guide coat stays put is a low spot. Fill it. Repeat until the surface sits flat.
Got pinholes or small voids? Use glaze filler and spread it edge-to-edge across the repair area. Keep it inside the featheredge. Let it cure hard, then blow off all dust before you start sanding.
Finish with a clear coat matched to the original surface — matte or gloss. Clean the surface with alcohol first. No exceptions.
How to Repair Specific Carbon Fiber Items (Scene-Based Mini Guides
Same process, different stakes. A scratch on a carbon bike frame needs more precision than a cosmetic scuff on a drone arm — because one of them breaks under 200 lbs of rider weight. Here’s how to use everything above on the items you’re most likely fixing right now.
Carbon Fiber Bike Frame
Match the weave direction before you touch anything else. Study the existing layup — note the angle, note the pattern — then cut your repair fabric to mirror it. First layer goes in at the same orientation as the original (say, 90°). Each layer after that alternates at 45°. This isn’t about looks. It’s how load distributes across a tube that flexes with every pedal stroke.
Taper your patches from small to large. Wrap compression tape tight over the wet layup. Clamp it. Use a heat gun to press the tape down — keep it moving so you don’t burn through. Once cured: wet sand with 120-grit, blend through 220, finish at 320.
The payoff: tubes repaired this way test as strong — sometimes stronger — than the originals. That’s not a rare result. It holds up in testing across repair types.
Carbon Fiber Drone Frame / Body Panel
Cosmetic damage on drone frames tends to be minor matrix cracking or surface delamination from a hard landing. Start by removing all damaged material, including the surrounding clear coat. Get down to clean fiber. Put on a sealing resin coat, let it tack up, then add your structural layers. Don’t stack too many flow coats — each extra layer means more sanding on a part with tight geometry.
One caution: sand slow. Hard passes on thin drone panels cut straight through into the substrate faster than you’d think. Light pressure, let the grit do the work, and check your depth often.
How Strong Is a Repaired Carbon Fiber Part? (Results & Expectations)

The honest answer is better than most people expect — and more complex than most repair guides admit.
A good multi-layer overlap repair gets back 80–100% of original structural strength in CFRP parts. That’s not marketing. That’s documented material science. Three things decide whether you land closer to 80% or 100%: resin selection, number of layup layers, and cure method.
What the data shows:
-
Vacuum curing beats hand layup — fewer internal voids, better resin spread, stronger finished laminate
-
Epoxy resin paired with high-tensile pre-impregnated fibers gives you stronger bonding at the interface
-
CFRP laminates in repair work have measured tensile strength of 724 MPa with a Young’s modulus of 56.5 GPa — these are solid numbers, not degraded ones
Long-term performance holds up too. A 12-year field study tracking bridge CFRP U-wrap repairs predicted 75% tensile strength retention at 75 years. That’s a real structure under real load, real weather, real time.
There are limits worth knowing. After 224 days of wet/dry cycling, tensile capacity drops about 33% and elastic modulus can fall by up to 26%. Schedule a re-inspection any time your repaired part faces heavy moisture exposure, fire damage, or loads above 80% of original capacity.
One hard ceiling: cyclic fatigue. CFRP’s fatigue limit under repeated loading sits around 10% of aluminum 6061 equivalent. For parts that flex non-stop — crank arms, suspension links — repair buys you time, not a permanent fix. Know what you’re asking the part to do.
Carbon Fiber Repair Cost: DIY vs Professional Service

Professional carbon fiber repair costs real money. The numbers also vary more than most people expect.
Surface scratches run $350–$450. Small cracks climb to $400–$600. Major fractures? Expect $700–$1,200 or higher. Component type matters too. Steering wheels hit $600–$1,200. Hoods and spoilers land at $500–$1,000. Interior trims fall in the $400–$750 range.
DIY kits cost under $300. That gap looks attractive — until you see what can go wrong.
Where DIY works:
– Surface scratches and cosmetic chips
– Non-structural trim pieces and decorative accessories
Where professional repair is the right call:
– Structural parts under load (hoods, steering wheels, panels)
– Internal delamination that needs injection repair
– Fiber fractures that need heat curing and NDT inspection
The failure points in DIY are easy to predict: wrong resin type, skipped vacuum bagging, rushed cure times, poor surface prep. Any one of these turns a $300 fix into a full replacement bill. Those parts cost $500–$5,000+ to replace outright.
The math is simple. Professional repair at $350–$1,200 beats replacement in almost every case. DIY makes sense for cosmetic damage on parts with zero structural load. Anything beyond that, go professional.
Common Carbon Fiber Repair Mistakes (And How to Avoid Them)

Most failed repairs share a common thread — not bad luck, but skipped steps.
Here are the mistakes that actually matter:
-
Missing hidden damage. A surface crack often hides delamination underneath. Visual inspection alone won’t catch it. Run a coin-tap test first. For structural parts, use ultrasound or thermography before touching anything.
-
Wrong resin for the job. Mismatched adhesives create weak bonds. They look fine — until they fail. Check the datasheet. Run a small compatibility test before committing to a full application.
-
Skipping proper surface prep. Grease, wax, and dust kill adhesion without any warning signs. Clean the surface well. Sand it down. Wipe with alcohol. Let it dry before moving on.
-
Leaving backing paper in pre-preg layers. One missed sheet of protective paper buried in your layup causes delamination from the inside out. Check every layer before it goes down. Don’t rush this step.
-
Going DIY on structural damage. Surface scratches are fair game for DIY. Cracks, delamination, and punctures are a different story. You need vacuum bagging or autoclave curing for those. A wet layup on a load-bearing part can look solid but fail in ways you won’t expect.
The fix is always the same: slow down at each step, and don’t assume the surface tells the whole story.
Conclusion
Carbon fiber isn’t forgiving — but it is fixable.
A hairline crack on a bike frame or a stress fracture on a body panel — both come down to three non-negotiables: proper damage assessment, clean surface prep, and quality epoxy resin. Skip one, and the repair fails. Nail all three, and you get a carbon fiber patch that restores structural integrity — at a fraction of what a professional shop charges.
The difference between a repair that holds and one that doesn’t isn’t talent. It’s patience and the right materials.
So here’s your next move:
-
Check your damage type using the assessment guide above
-
Gather your tools before you start
-
Start small if this is your first repair
Contact HyperX Carbon – Your Trusted Chinese Carbon Fiber Partner
Ready to source high-performance carbon fiber materials or custom forged carbon fiber parts from China?
HyperX Carbon is a leading manufacturer with 20+ years of expertise, specializing in aerospace-grade forged carbon fiber, prepreg, tubes, sheets, and lightweight automotive/drone/medical components. We offer:
-
Stable supply chain with premium raw materials (Toray, Mitsubishi, Hengshen)
-
AS9100D certified production for aerospace & UAV applications
-
Rapid prototyping (5-8 weeks) and monthly capacity exceeding 180,000 parts
-
Competitive pricing with 15-18% cost savings on forged carbon solutions
-
Full customization: from T700/T1100G to ultra-high modulus grades
Whether you’re an eVTOL developer, automotive OEM, drone manufacturer, or medical device engineer, HyperX delivers consistent quality, batch-to-batch reliability, and reliable delivery.
Get in touch today for a free consultation, custom quote, or material sample.
📧 Email: [email protected]
🌐 Website: https://www.hyperxcarbon.com/
📞 Phone/WhatsApp: +86 15623270276 (English support available)
Let’s build your next lightweight innovation together – contact HyperX Carbon now and stay ahead in the low-altitude and advanced composites market.